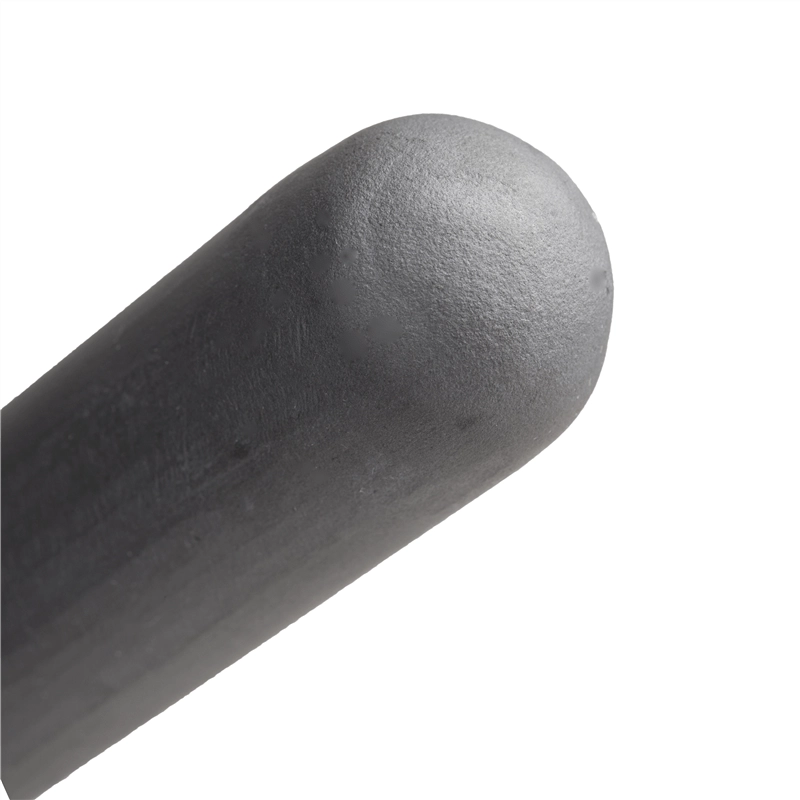
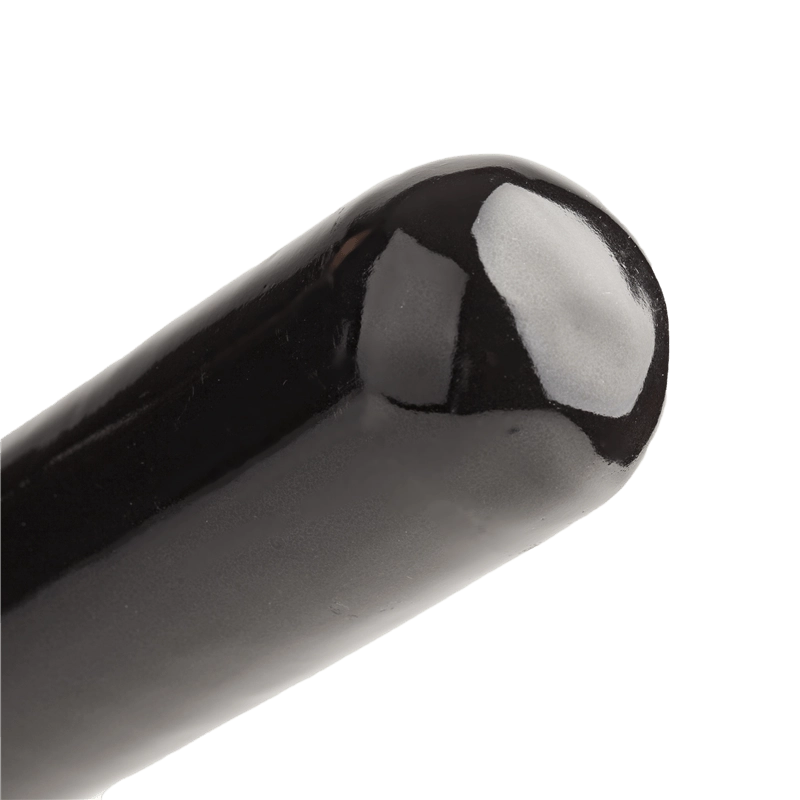
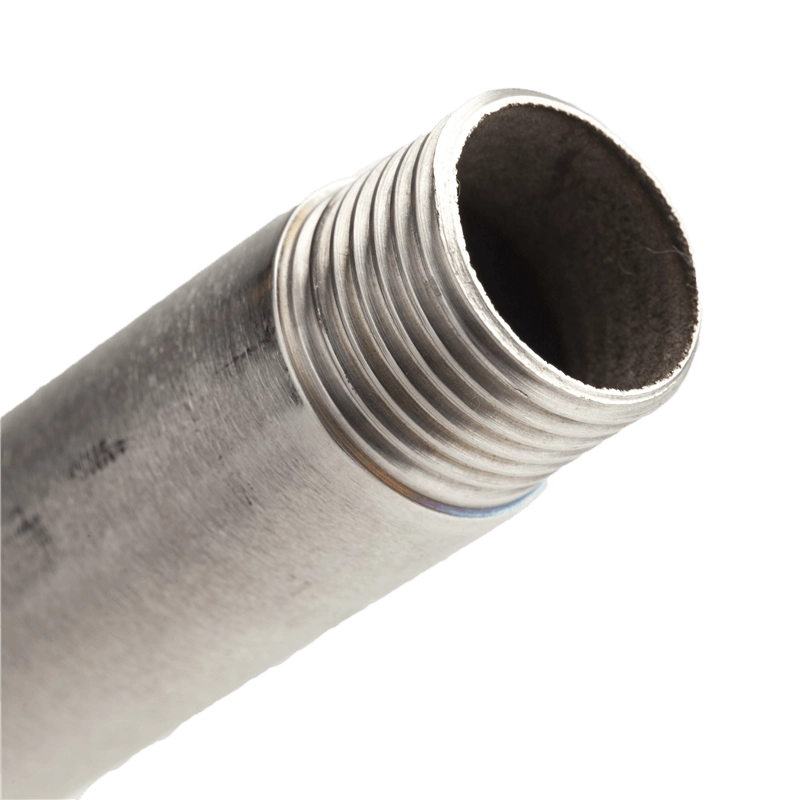
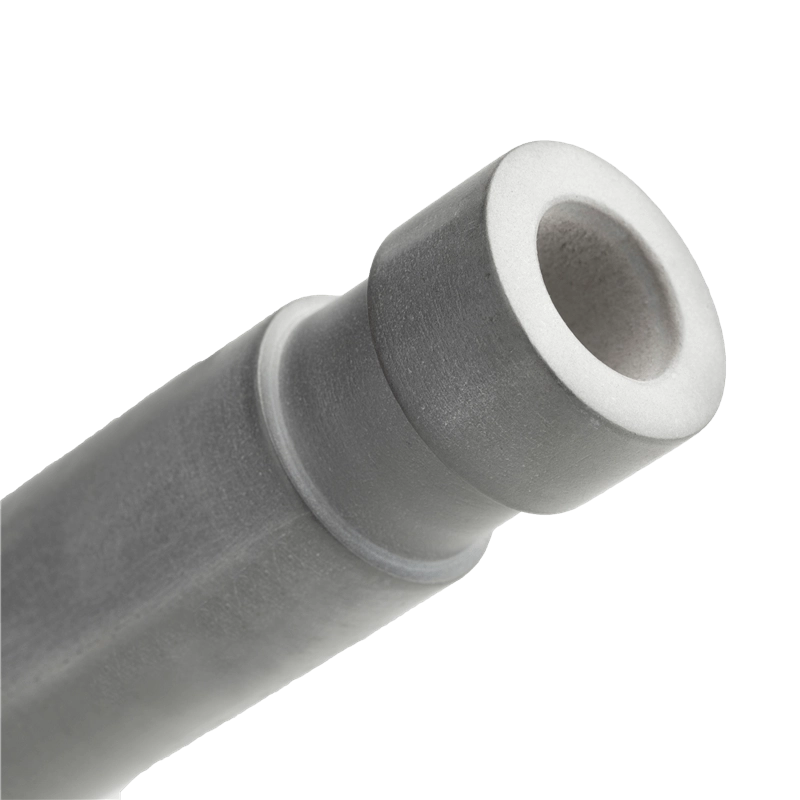
Alumina and sillimanite tubes and components are used to protect sensors in industrial high-temperature applications requiring dimensional stability and insulation under demanding operating conditions. These technical ceramics help protect thermocouples and other components against direct exposure to gases, wear, contamination and aggressive environments.